Precision quartz vessels, oversized diffusion tubes, and high-purity thermal carriers engineered for continuous duty in extreme semiconductor, photovoltaic, and laboratory thermal regimes.
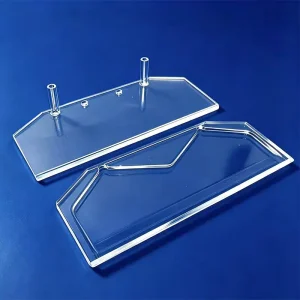
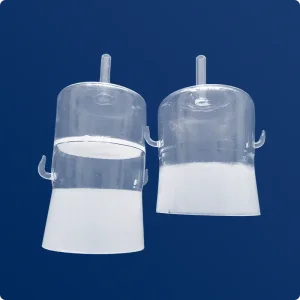
In high-temperature pyrometallurgy, semiconductor wafer crystallization, and photovoltaic ingot casting, determining the maximum operational temperature of a silica crucible requires examining phase transformation thermodynamics, viscous relaxation rates, and trace hydroxyl-alkali kinetics rather than a single static melting point.
Internal stresses relax completely over hours. Absolute threshold for zero-creep dimensional tolerance under physical loads.
Thermal stress relief occurs within minutes. Upper limit for continuous unsupported vertical crucible wall stability.
Viscous deformation occurs rapidly under self-weight. Physical shape collapses without external graphite susceptors.
Theoretical phase transition to liquid SiO₂. High viscosity preserves structural form over short intervals.
Fused silica is a metastable, amorphous allotrope of silicon dioxide. When exposed to temperatures above 1150°C, the amorphous glass network undergoes a reconstructive phase transformation into crystalline β-cristobalite. As the crucible cools past 270°C–200°C, β-cristobalite converts to α-cristobalite accompanied by a drastic volumetric contraction of 2.8% to 4.5%. This sharp volume change generates intense internal microcracks, leading to fatal thermal shock fractures (crazing).
The Catalytic Impact of Alkali Contamination: Nucleation and crystallization rates are heavily driven by monovalent alkali impurities (specifically Na⁺, K⁺, and Li⁺). Even surface contamination of < 5 ppm from fingerprint residue accelerates cristobalite growth rates by several orders of magnitude at 1200°C.
Hydroxyl groups (-OH) act as network terminators within the three-dimensional silicon-oxygen tetrahedral framework [SiO₄]. Each terminal OH bond severs a bridging oxygen atom (Si-O-Si), disrupting continuous structural connectivity and drastically lowering the molten silica's effective activation energy for viscous flow.
At our Donghai vacuum arc fusion facility, electric-melt fused silica maintains an ultra-low hydroxyl content (OH < 20 ppm to < 5 ppm for premium electro-fused crucibles), compared to flame-hydrolysis synthetic silica (which can contain 200–1000 ppm OH). Consequently, our high-purity industrial crucibles sustain continuous service at 1150°C to 1250°C without structural sag, and survive intermittent peaks up to 1450°C in inert atmospheres.
Free-standing / Laboratory Regimes: In bench-top muffle furnaces or box reactors where crucibles rest unsupported, the strict continuous operational boundary is 1150°C (2102°F). Above this threshold, gravitational creep causes unreinforced sidewalls to bow outward or deform.
Czochralski (CZ) / Photovoltaic Pulling: Inside single-crystal CZ pulling pullers, silica crucibles operate at 1420°C to 1450°C (exceeding molten silicon’s melting point of 1414°C) because they are enclosed by precision-machined isostatic graphite susceptors, using hydrostatic molten silicon pressure against an exterior support shell.
Comprehensive thermodynamic and mechanical properties of Southeast Quartz high-temperature silica crucibles manufactured under ISO 9001 quality controls.
| Physical / Chemical Property | High-Purity Arc Fused Quartz (Standard) | Synthetic / Low-OH Fused Silica (Premium) | Test Standard / Engineering Method |
|---|---|---|---|
| Maximum Working Temperature (Continuous) | 1100°C – 1150°C | 1200°C – 1250°C | ASTM C623 / Static Creep Test |
| Maximum Working Temperature (Short-Term / Flash) | 1350°C – 1400°C | 1450°C – 1500°C | Vacuum Thermal Sag Evaluation |
| Softening Point (log₁₀ η = 7.6) | 1683°C (3061°F) | 1710°C (3110°F) | ASTM C338 Standard Fiber Elongation |
| Annealing Point (log₁₀ η = 13.0) | 1215°C (2219°F) | 1250°C (2282°F) | ASTM C336 Fiber Elongation Method |
| Strain Point (log₁₀ η = 14.5) | 1075°C (1967°F) | 1120°C (2048°F) | ASTM C336 Standard Test |
| Mean Coefficient of Thermal Expansion (CTE) | 5.5 × 10⁻⁷ / K (20°C – 1000°C) | 5.2 × 10⁻⁷ / K (20°C – 1000°C) | Dilatometry / Thermal Expansion Rig |
| Chemical Purity (SiO₂ Concentration) | ≥ 99.99% (4N) | ≥ 99.999% (5N) | Inductively Coupled Plasma Mass Spectrometry (ICP-MS) |
| Hydroxyl Group Concentration ([OH⁻]) | < 30 ppm (Electric Arc Fused) | < 5 ppm (Vacuum Degassed) | FTIR Infrared Spectroscopy (2.73 µm band) |
| Thermal Shock Resistance | Quench from 1100°C to 20°C cold water without rupture | Quench from 1200°C to 20°C water without rupture | Rapid Cyclic Water Quenching Test |
| Compressive Strength (20°C) | 1150 MPa | 1200 MPa | Hydraulic Mechanical Load Testing |
The international supply chain for industrial crucibles is navigating an unprecedented structural transformation. Stringent purity specifications from 300mm sub-3nm semiconductor fabricators, multi-gigawatt N-type solar capacity additions, and next-generation battery calcination processes dictate new mechanical and thermal criteria for B2B buyers across Europe, North America, and East Asia.
The global solar sector’s mass migration from P-type PERC to N-type TOPCon and Heterojunction (HJT) wafers has driven up silicon melt temperatures and lengthened thermal hold cycles to over 300 continuous hours.
Silicon crystal growers now specify 32-inch, 36-inch, and 40-inch large-diameter quartz crucibles with bubble-free synthetic inner liners that resist microscopic peeling at 1450°C, mitigating oxygen and dislocation contamination during crystal growth.
Modern 300mm fabs running 3nm, 2nm, and gate-all-around (GAA) logic architectures demand parts-per-billion (ppb) chemical purity.
Crucibles used in synthetic quartz feedstock fusion, compound semiconductor growth (GaAs, InP), and LPCVD/diffusion lines require complete absence of aluminum, iron, and boron dopants to preserve dielectric gate insulation and carrier mobility.
Electrode Induction Melting Gas Atomization (EIGA) and vacuum induction melting (VIM) for aerospace-grade nickel, titanium, and cobalt superalloy powders rely on fused silica crucibles.
Thermal engineers prioritize molten metal non-wettability, absence of iron-oxide inclusions, and extreme thermal-shock endurance against molten metal streams at 1350°C–1400°C without crucible spalling.
Lianyungang Southeast Quartz Products Co., Ltd. is located in Donghai County, Jiangsu—the premier quartz processing cluster in the Eurasian industrial corridor. We unite domestic and global supply security with high-throughput automated manufacturing, rigorous non-destructive inspection, and drawing-to-prototype production cycles.
Direct proximity to top-tier high-purity natural silica deposits combined with integrated chlorination-purification refining facilities. We maintain over 3,000 metric tons of stabilized raw quartz tube, rod, plate, and ingot inventory, insulating our international partners from supply-chain interruptions.
Advanced robotic centrifugal electric arc fusing chambers paired with 5-axis CNC diamond ultrasonic grinding centers. We achieve sub-micron wall thickness uniformity, strict concentricity on crucibles up to 48 inches OD, and automated laser-controlled edge fire-polishing to eliminate microcrack propagation.
Every pressure-bearing quartz unit, vacuum bell jar, and thermal crucible undergoes rigorous non-destructive evaluation: helium leak testing down to 1 × 10⁻¹⁰ mbar·L/s, stress polarimetry inspection, ultrasonic wall verification, and full-spectrum ICP-MS lot-traceable metallurgical certification.
How process engineers prevent early thermal failure across demanding high-temperature environments.
Operating Environment: Vacuum envelope (~10 to 30 Torr Argon purge), direct contact with molten polycrystalline silicon at 1420°C for runs exceeding 150–300 hours.
Engineering Solution: We engineer a specialized dual-layer crucible. The outer layer consists of high-density opaque fused quartz with high thermal insulation and bubble density to diffuse radiative heat uniformly. The inner layer is formed from high-purity synthetic transparent silica (thickness 1.5–3.0 mm, micro-bubble count < 50/cm³) that resists thermal dissolution into the melt (Si + SiO₂ → 2SiO↑), minimizing pinhole formation and silicon leakage.
Operating Environment: Rapid RF induction heating of gold, silver, platinum, palladium, and cobalt-chromium alloys under normal air or protective argon environments.
Engineering Solution: Fused silica’s thermal expansion coefficient (5.5 × 10⁻⁷ / K) allows these crucibles to survive rapid thermal cycling—from 20°C ambient to 1300°C within 60 seconds without cracking. Pre-firing at 1000°C to strip surface moisture and using clean ceramic tongs prevent localized thermal gradients and premature devitrification.
Operating Environment: Synthesis of high-nickel ternary cathode precursors (NCM/NCA) and sulfide/oxide solid-state electrolytes in oxidizing atmospheres.
Engineering Solution: Molten lithium salts (LiOH, Li₂CO₃) corrode conventional alumina (Al₂O₃) or mullite saggers, forming aluminates and flaking debris. Our acid-leached high-purity fused silica crucibles and saggers offer stable resistance against lithium vapor attack below 1100°C, lowering metallic cross-contamination to sub-1 ppm.
Operating Environment: SiC/GaN epitaxy, wafer diffusion, and low-pressure chemical vapor deposition (LPCVD) utilizing corrosive precursors (SiH₄, BCl₃, POCl₃, HCl) at 1000°C–1200°C.
Engineering Solution: Fused quartz is chemically inert to virtually all acids (except hydrofluoric and concentrated hot phosphoric acid above 300°C). Our custom flanged reactors, slotted quartz boats, and bell jars maintain gas-tight seal integrity under aggressive thermal cycling and vacuum.
Clear engineering answers regarding thermal limits, devitrification prevention, and ordering procedures for industrial buyers.
Customized fused silica components built to drawing specifications, rigorously inspected with helium mass spectrometry leak testing and optical spectroscopy.
Work directly with our senior quartz engineers in Donghai County, China. Provide your operational temperature, required tolerances, chemical environment, or custom drawing files (PDF, DWG, STEP) for an engineering review and direct factory quote within 24 hours.