Factory-direct fused quartz fabrications engineered to DIN/ASTM tolerances with total impurity levels < 15 ppm, designed for continuous operation at 1,150°C and transient thresholds reaching 1,300°C.
Analyzing global demand trajectories, chemical refinement advancements, and microstructural demands reshaping high-performance fused quartz manufacturing.
In modern industrial physics and semiconductor microfabrication, fused quartz (SiO₂ ≥ 99.99%) stands as an irreplaceable substrate. As sub-5nm lithography nodes, large-area silicon carbide (SiC) epitaxy, and next-generation TOPCon photovoltaic technologies mature, thermodynamic and chemical demands placed on hot quartz components have escalated dramatically. The global market has ceased treating quartzware as simple furnace glassware; instead, enterprise procurement teams treat quartz furnace tubes, wafer carriers (quartz boats), and bell jars as critical process chamber liners directly influencing wafer yield and cycle-time repeatability.
According to current supply-chain research, three macro vectors are driving technological capital expenditure in the quartz glass sector:
Diffusion processes running above 1,100°C trigger exponential mobility of metallic dopants. Traditional electric-fused quartz with 30-50 ppm bulk impurities is obsolete. Contemporary semiconductor-grade fabrications demand cumulative alkali-metal (Li, Na, K) limits below 1.5 ppm and transition metals (Fe, Cu, Ni) below 1.0 ppm to eliminate crystal lattice poisoning.
From M10 to G12 solar wafers and 300mm silicon ingots, process geometries have surged. Furnace tubes now require outer diameters (OD) exceeding 450mm to 650mm with lengths beyond 2,500mm. Producing oversized fused quartz tubes with uniform radial wall thickness tolerances within ±0.2mm without sagging demands cutting-edge continuous electric-fusion and precision plasma lathe integration.
Thermal fatigue remains the primary operational cost for high-temperature diffusion furnaces. High-hydroxyl (OH) content lowers quartz viscosity, accelerating transition into crystalline cristobalite at 1,150°C. By executing synthetic thermal refining and vacuum dehydroxylation, manufacturers drive OH- levels under 10-20 ppm, multiplying component lifespan 2.4-fold.
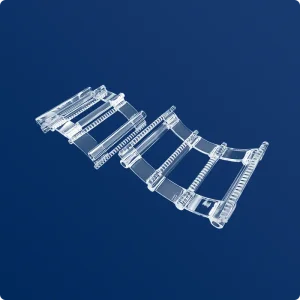
Modern slotted quartz boats require slot pitch accuracy within ±0.03mm to accommodate automatic robotic end-effectors without wafer edge chipping. Flame welding transitions are inspected via polariscopic stress analyzers to ensure residual stress does not exceed 10 MPa, eliminating microcracking during repetitive rapid-thermal cycles.
Essential inspection criteria for global engineering teams sourcing high-temperature fused quartz vessels, structural components, and optical plates.
Purchasing directors and fab engineering teams face severe operational risks when procuring quartzware. A micro-fracture under vacuum or heavy metal volatilization in a 1,200°C furnace can ruin full batches of semiconductor silicon wafers, causing hundreds of thousands of dollars in downtime. Sourcing organizations must mandate exhaustive lot-traceable verification protocols.
| Evaluation Parameter | Standard Laboratory Spec | Semiconductor Production Spec | Diagnostic / Testing Methodology |
|---|---|---|---|
| Trace Alkali Impurities (Li, Na, K) | < 5.0 ppm | < 1.0 ppm (Aggregated) | Inductively Coupled Plasma Mass Spectrometry (ICP-MS) |
| Hydroxyl Radical Concentration (OH⁻) | < 150 ppm | < 15 – 30 ppm | Fourier-Transform Infrared Spectroscopy (FTIR, 2.73 μm absorption) |
| Annealing Point / Strain Point | 1,120°C / 1,025°C | 1,180°C / 1,075°C | Beam Bending Viscometry (ASTM C598 / DIN 52312) |
| Surface Bubble & Inclusion Density | ISO 10110-3 Class 2 | ISO 10110-3 Class 0 (Zero bubbles > 0.05mm) | Laser Scattering Tomography / Automated Optical Inspection (AOI) |
| Vacuum Hermetic Tightness | 1.0 × 10⁻⁷ mbar·l/s | < 1.0 × 10⁻⁹ mbar·l/s | Helium Mass Spectrometry Sniffer / Hard Vacuum Chamber Sniffing |
| Residual Optical Stress | ≤ 25 nm/cm | ≤ 8 – 10 nm/cm | Dual-Refraction Polarimetry (Sénarmont Compensator Method) |
Translating material physics into uptime and structural stability across semiconductor, solar photovoltaic, optical instrumentation, and chemical sectors.
In low-pressure chemical vapor deposition (LPCVD), thermal oxidation, and boron/phosphorus diffusion, our oversized quartz tubes and multi-slot quartz boats deliver unmatched thermal stability. They resist corrosive etch chemistries while preventing thermal gradient shock during rapid push-pull cycles, protecting sub-nanometer thin films.
Modern N-type TOPCon and HJT solar lines operate at high throughput with stringent cost-per-watt targets. We manufacture extra-long furnace tubes (up to 3,000mm) and high-load wafer boats capable of handling heavy mass loading without warp, lowering maintenance cycle intervals in POCl3 diffusion chambers.
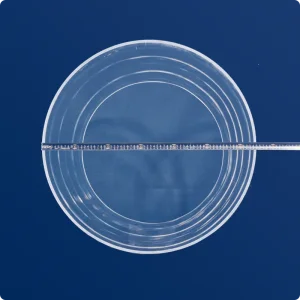
Fused silica optical plates and microchannel flow cells provide over 92% optical transmission from 200 nm deep-UV through the near-infrared spectrum (2,500 nm). Free of striae, internal bubbles, and fluorescence background, these components form the backbone of high-precision spectrophotometry, laser optics, and flow cytometry.
Our gold-coated and half-white reflective quartz heating lamp holders and infrared tubes convert up to 95% of electrical energy into directed electromagnetic radiation. Excellent mechanical resistance ensures stability in high-vibration plastic blowing, composite curing, and automotive coating drying tunnels.
Integrated manufacturing workflows located in Donghai County, Jiangsu — connecting direct raw material supply to CNC machining and certified leak verification.
Lianyungang Southeast Quartz Products Co., Ltd. operates a vertically integrated production campus spanning more than 25,000 square meters. By sourcing premium natural crystalline silica directly from China’s leading mineral hub in Donghai and processing plasma-fused ingots in-house, we eliminate external intermediary markups while maintaining complete raw material purity traceability.
Equipped with 4-axis and 5-axis ultrasonic CNC grinding centers, high-speed diamond wafer saws, and abrasive waterjet profiling tables. We machine complex slots, step-cut flanges, blind holes, and irregular optical window contours with dimensional repeatability within ±0.01 mm.
Our heavy-duty quartz glassblowing lathes support pipe processing up to 750mm OD. Utilizing oxy-hydrogen burner manifolds with digital proportional gas mixing, our artisans and robotic fixtures execute automated bubble-free joints, dome closures, and ground glass flange fusions with zero localized crystallization.
Following machining and hot fusion, components undergo multi-stage acid washing using automated ultrasonic baths filled with high-purity hydrofluoric (HF) and nitric (HNO₃) acid blends. This strip removes iron residue, surface micro-cracks, and volatile organics before cleanroom thermal annealing.
Quartz components are protected inside cleanroom-grade antistatic packaging, suspended in engineered closed-cell high-density polyethylene (EPE) foams, and sealed inside fumigated structural plywood crates. Sensitive oversized orders include continuous shock and tilt telemetry monitors.
Strategic technological initiatives driving Southeast Quartz through the next evolution of deep-UV photolithography, 300mm wafer expansions, and advanced photonic applications.
Transitioning from natural quartz crystal to synthetic silicon tetrachloride (SiCl₄) cracking. Synthetic fused silica eliminates mineral impurity limits, driving purity to 6N–7N (99.99999%), eliminating deep-UV excimer solarization in laser window applications.
Engineering electric vacuum heating systems capable of drawing quartz processing chambers beyond 800mm in diameter, engineered to support 300mm wafer batch LPCVD processing and large-scale semiconductor etching equipment.
Developing specialized quartz variants doped with Titanium (UV-blocking), Cerium (radiation-hardened), or rare earths to filter harmful emission spectra in industrial photopolymerization and aerospace sensors.
Addressing core procurement inquiries, operating boundaries, chemical handling parameters, and mechanical tolerances for fused quartz components.
To produce an authoritative technical quote and manufacturing evaluation within 24 hours, provide: 1) Tube OD, ID, and wall thickness tolerance (e.g., OD 300mm ± 0.5mm, WT 5.0mm ± 0.3mm); 2) Overall length and straightness limits (< 1.5mm per meter standard); 3) End geometry details (flat flame-cut, ground perpendicular, flanged, O-ring groove, or standard ball-and-socket ground joints); 4) Purity grade requirement (High-purity natural silica vs. Synthetic silica); 5) Operating atmosphere (vacuum, reducing H₂, or oxidizing gas flow) and sustained operating temperature; and 6) 2D PDF blueprints with critical dimensional datums and native 3D STEP/DWG models.
Devitrification is the phase transformation of metastable amorphous fused silica into crystalline cristobalite. It generally initiates above 1,150°C and is sharply accelerated by surface contaminants, particularly alkali metal ions (Na⁺, K⁺, Li⁺, Ca²⁺) found in tap water, sweat, and airborne dust. Cristobalite has a different thermal expansion coefficient than fused quartz; during thermal cooldown past 270°C, the cristobalite undergoes volumetric shrinkage, inducing micro-cracking and eventual spalling. To maximize operating life: always handle quartz components using cleanroom nitrile gloves, rinse only with high-resistivity deionized water (18.2 MΩ·cm), perform periodic 5–10% hydrofluoric (HF) acid washes to strip nucleating surface layers, and purge processing atmospheres with ultra-pure dry nitrogen or argon.
Electric-fused quartz is manufactured by melting high-purity natural silica sand in tungsten or molybdenum electrical resistance furnaces. It offers exceptionally low hydroxyl (OH⁻) content (< 20–30 ppm), resulting in superior structural viscosity, higher annealing points, and elevated resistance to sagging at sustained continuous temperatures (up to 1,150°C). Flame-fused quartz is melted using oxy-hydrogen burners; it contains higher OH⁻ levels (150–250 ppm), which moderately reduces high-temperature creep resistance but produces virtually bubble-free glass with superior optical homogeneity and lower bubble inclusion counts, making it ideal for precision optical windows, bell jars, and analytical cuvettes.
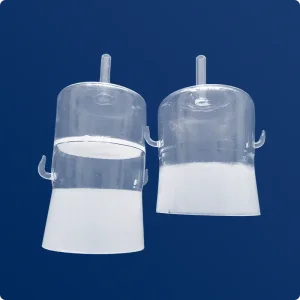
All fabricated quartz vessels, bell jars, source bottles, and flanged reaction tubes undergo a rigorous 4-step quality assurance gate: 1) Polariscopic optical stress evaluation to verify that hot-welded seams have been fully annealed down to < 10 MPa residual strain; 2) Helium mass-spectrometry leak detection in hard-vacuum mode, ensuring leak rates stay strictly below 1.0 × 10⁻⁹ mbar·l/s; 3) Hydrostatic or pneumatic pressure proof-testing up to 1.5× the rated chamber operational working pressure; and 4) Coordinate Measuring Machine (CMM) dimensional verification against the client's engineering print.
Yes. Every production run is linked to batch-specific raw quartz sand and plasma ingot assay records. On demand, shipments are accompanied by third-party testing reports (such as SGS, National Glass Inspection Center) certifying elemental impurity levels across 16 elements via ICP-MS, compliance with EU RoHS and REACH frameworks, and non-radioactivity certs. Full material safety and specification compliance documentation are standard inclusions for our tier-1 global semiconductor and laboratory accounts.
Direct supply line for custom-ground quartz rings, optical plates, high-efficiency lamp holders, and solid fused silica rods tailored for OEM manufacturing and precision laboratories.