Explore standard and customizable fused quartzware, furnace tubes, and precision-slotted wafer boats engineered to withstand temperatures up to 1,250 °C with minimal structural devitrification.
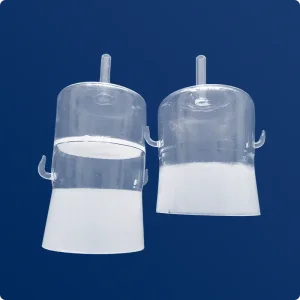
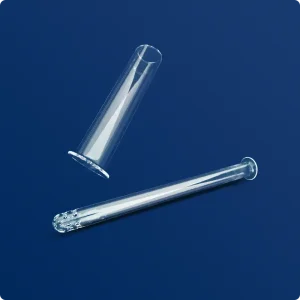
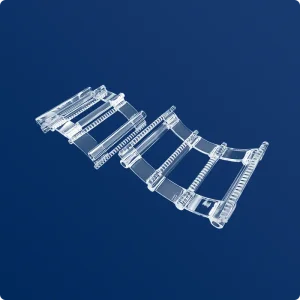
Strategic analysis of critical thermal carrier consumables across advanced 200mm/300mm semiconductor fabs, next-generation compound semiconductors, and N-type photovoltaic cell production lines.
In modern microelectronics and high-efficiency photovoltaic manufacturing, the wafer carrier quartz boat (also designated across international cleanroom facilities as a quartz cassette, quartz ladder, or slotted wafer carrier) occupies an indispensable position within the front-end thermal processing equipment architecture. As integrated circuit lithography scales beyond deep sub-micron nodes and photovoltaic architectures migrate en masse from P-type PERC toward N-type TOPCon and Heterojunction (HJT) technologies, the thermal and chemical resilience of quartz boats dictates wafer throughput, batch uniformity, and yield reliability.
The global demand for high-purity quartz boats is primarily catalyzed by horizontal diffusion furnaces, vertical low-pressure chemical vapor deposition (LPCVD) reactors, atomic layer deposition (ALD) chambers, and rapid thermal processing (RTP) assemblies. During thermal oxidation and dopant diffusion processes—frequently operating between 900 °C and 1,200 °C in corrosive halide and oxygen atmospheres (such as POCl₃, BBr₃, HCl, and wet O₂)—ordinary metallic or ceramic fixturing suffers severe catastrophic degradation, micro-particle spalling, or unacceptable heavy-metal ionic outgassing. High-purity fused silica (fused quartz) remains the universal benchmark material due to its near-zero coefficient of thermal expansion (5.5 × 10⁻⁷ / °C), remarkable thermal shock tolerance, superior chemical inertness against concentrated inorganic acids, and transparent crystalline integrity.
Information Gain Insight: The transition from 150mm/200mm legacy wafers to 300mm ultra-thin substrates has revolutionized quartz boat mechanical design. In vertical ladder assemblies, gravitational stress on wafer contact notches induces edge slip and micro-twinning under sustained thermal loads. Engineering modern quartz boats requires dynamic thermal finite-element analysis (FEA), high-precision flame-welded structural junctions, and robotic slot pitch tolerances calibrated to sub-hundred-micron margins to integrate seamlessly with automated material handling systems (AMHS).
On a macro-industrial scale, international fab operators across North America, Europe, Taiwan, South Korea, and Japan face escalating supply chain constraints, prolonged lead times, and prohibitive procurement margins from traditional domestic glassblowers. Sourcing directors and tool integration engineers increasingly leverage qualified direct-manufacturer ecosystems in China, where advanced computerized CNC cold-grinding, plasma hot-flame fusion, and raw material purification clusters deliver unparalleled supply chain continuity and substantial capital expenditure reductions.
How deep raw material vertical integration, ultra-precision cold-machining CNC capabilities, and master glassblowing craftsmanship create exceptional commercial velocity for global buyers.
Situated within Donghai County—the epicenter of the Eurasian quartz industrial network—our facility secures verified natural quartz crystal and high-purity synthetic SiO₂ feedstock with immediate proximity, eliminating logistical latency and raw-stock markups.
Every wafer support rod undergoes automated multi-axis diamond slot grinding. This proprietary mechanical slotting workflow ensures micro-groove tolerances of ±0.03mm, smooth radius transitions, and zero micro-cracking along notch contact surfaces.
While computer automation cuts and slots rods with absolute fidelity, the welding of quartz cross-beams, handles, and end-caps demands veteran master glassblowers. Our factory combines hydrogen-oxygen burner manipulation with precise lathe-guided fixturing.
The manufacturing efficiency of Southeast Quartz is rooted in complete vertical autonomy. Traditional Western and regional suppliers frequently subcontract ingot slicing, slotting, and flame fusion to disjointed regional workshops, compounding cumulative lead times to 16–26 weeks. By unifying continuous electric fusion ingot drawing, computer-controlled cold diamond slicing, cleanroom acid pickling, thermal de-stress annealing, and ISO-certified mass-spectrometric leak testing under a single enterprise roof, our factory achieves prototype validation within 10 business days and volume production batches within 3 to 4 weeks.
Furthermore, local supply chain integration directly dampens cost volatility. High-purity fused silica tubing—used for carrier side rails and handling rods—is manufactured adjacent to our assembly lines. This closed-loop fabrication infrastructure enables rapid tooling adjustments for non-standard wafer pitch designs, custom semiconductor test fixtures, and large-format solar batch carriers without imposing custom tooling surcharges.
Comparative architectural taxonomy and operational limits across horizontal diffusion, vertical LPCVD, wet chemical etching, and PV industrial processes.
| Architecture Type | Primary Thermal Process | Typical Wafer Capacity | Operating Temp Range | Critical Engineering Focus |
|---|---|---|---|---|
| Horizontal Diffusion Boat | POCl₃ / BBr₃ Diffusion, Dry O₂ Oxidation | 50 – 100 Wafers / Boat | 850 °C – 1,180 °C | Cross-beam thermal expansion tolerance, slot angle precision, sag resistance. |
| Vertical Ladder Quartz Boat | LPCVD Poly-Si, Low-Temp Nitride, ALD | 100 – 150 Wafers / Stack | 450 °C – 1,050 °C | Vertical center-of-gravity balance, robot paddle automation slot pitch, zero micro-shake. |
| Solar High-Density Boat | TOPCon Boron Diffusion, Tube PECVD | 150 – 400 Wafers / Train | 750 °C – 1,000 °C | Ultra-thin slot pitch (down to 1.2mm), mechanical shock survival, rapid load cycling. |
| Wet Chemical Etching Carrier | Acid Etch (HF, HNO₃, Piranha), RCA Clean | 25 – 50 Wafers | Ambient – 140 °C | Perforated bottom geometry for fluid dynamics, zero static acid entrapment pockets. |
| Compound Semi Carrier (GaAs/SiC) | Epi-layer Annealing, Sintering | Single to 25 Wafers | 900 °C – 1,250 °C | Zero metallic outgassing (Cu, Fe, Ni < 0.05 ppm), inert synthetic silica matrix. |
During prolonged thermal exposure exceeding 1,100 °C, fused silica naturally tends toward thermodynamic equilibrium by restructuring into crystalline α-cristobalite. This phenomenon—known as devitrification—initiates predominantly at surface micro-imperfections, microscopic particulate nucleating sites, or areas tainted with alkali metals (sodium, potassium, lithium). Once cristobalite forms, cooling through the 200 °C to 275 °C critical zone triggers a destructive volumetric phase inversion, causing micro-cracking, loss of structural rigidity, and hazardous particulate generation inside process chambers.
Southeast Quartz implements a rigorous anti-devitrification engineering protocol:
A comprehensive blueprint for engineering procurement teams evaluating quartz boat vendors against rigorous SEMI, ISO, and tier-one semiconductor standards.
Inductively Coupled Plasma Mass Spectrometry (ICP-MS) verification guaranteeing that transitional elements (Fe, Cu, Ni, Cr) and mobile alkali ions (Na, K, Li) remain under 0.1 ppm total concentration to eliminate gate-oxide breakdown risks.
Strict geometric fidelity with SEMI E1.9 standard carrier interfaces. Precise notch depth, bevel tolerances, and slot angle parallelism assure zero wafer slippage, misplacement, or sensor false-alarms on automated loading paddles.
Computer-simulated finite element modeling ensures weld fillets and ladder cross-bars absorb repetitive thermal cycling from room temperature to 1,200 °C without warping, buckling, or initiating fatigue fracture lines.
Multi-stage cleanroom megasonic deionized water scrubbing, drying under laminar HEPA flow, and double-vacuum containment with anti-static, cleanroom-certified polyethylene shielding to ensure zero inbound particle contamination.
To accelerate custom quartz boat fabrication and avoid iterative engineering revisions, global equipment manufacturers and fab operations managers should submit the following parameters with their request for quotation (RFQ):
In-depth responses covering material properties, cleaning protocols, service lifespan extension, and wholesale ordering policies.
Explore additional certified fused quartz components, large-diameter process tubes, and industrial quartz assemblies crafted to your precise equipment blueprints.
Send your CAD drawings, dimensional specifications, or process gas parameters. Our engineering department reviews manufacturability, confirms purity grades, and issues a formal technical quotation within 24 hours.