Engineered for cleanroom deployment in wafer fabrication, thermal epitaxial processing, and high-temperature vacuum isolation across British industrial hubs.
Strategic material alignment for Newport Wafer Fab, CSconnected South Wales, Silicon Glen, and Oxford/Cambridge deep-tech ecosystems.
With the UK government's commitment of £1 billion under the National Semiconductor Strategy, Britain is accelerating its specialization in compound semiconductors, silicon photonics, RF telecommunications, and advanced power electronics. Regional clusters—spanning the Newport-Cardiff corridor in South Wales (the world's first compound semiconductor cluster), the "Silicon Glen" corridor across central Scotland, and the photonics clusters in Southampton and Cambridge—are running high-density plasma etch, chemical vapor deposition (CVD), and metal-organic chemical vapor deposition (MOCVD) systems at capacity.
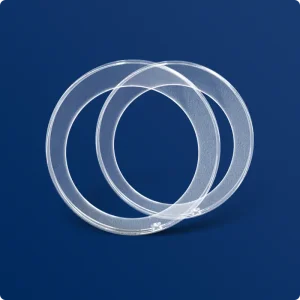
In these environments, custom quartz rings (focus rings, clamp rings, plasma containment rings, and gas distribution rings) are not passive glass consumables; they are critical process-control consumables. A minor deviation in trace element contamination (such as Fe, Cu, or Na exceeding 0.1 ppm) or an eccentricity mismatch above 10 microns can trigger premature wafer micro-arcing, uneven etching rates across 150mm and 200mm wafers, and devastating yield losses.
Evaluating trace impurity spectra, mechanical resilience, and hydroxyl radical (OH) concentrations for British process engineers.
| Physical / Chemical Parameter | Standard Electric Fused (Grade A) | Oxy-Hydrogen Flame Fused (Grade SG) | Synthetic Fused Silica (Ultra-Pure) | Engineering Benefit to UK Fabs |
|---|---|---|---|---|
| SiO₂ Purity Percentage | ≥ 99.99% | ≥ 99.998% | ≥ 99.9999% (6N) | Eliminates deep-level metallic traps in silicon/GaN epi |
| Hydroxyl [OH⁻] Content | < 5 – 20 ppm | 150 – 200 ppm | < 1 ppm (Dry) to 1000 ppm (Wet) | Controls thermal viscosity & IR transmission stability |
| Coefficient of Thermal Expansion | 5.5 × 10⁻⁷ / K (20–320°C) | 5.5 × 10⁻⁷ / K (20–320°C) | 5.1 × 10⁻⁷ / K (20–320°C) | Near-zero thermal shock rupture during rapid thermal processing (RTP) |
| Total Metallic Impurities (Al, Fe, Cu, Ti) | < 18.5 ppm | < 8.0 ppm | < 0.1 ppm total | Prevents chamber cross-contamination during halogen plasma cycles |
| Softening Point (°C) | 1683°C | 1680°C | 1600°C | Structural integrity maintained under sustained vacuum loads |
| Annealing Point (°C) | 1215°C | 1180°C | 1120°C | Virtually zero mechanical creep during high-temp oxidation steps |
We execute complex chamfers, notched wafer alignment slots, step recesses, and O-ring sealing grooves with tolerances down to ±0.005mm without subsurface micro-fracturing.
Post-machining multi-acid pickling (HF/HNO₃ balance) eliminates mechanical stress points, rendering a surface roughness of Ra < 0.2 µm or specular fire-polished optical finish.
Every production batch shipped to British partners comes accompanied by Glow Discharge Mass Spectrometry (GD-MS) purity logs and 3D CMM coordinate verification reports.
Overcoming domestic UK supply bottlenecks through direct engagement with the world's epicentre of quartz refining and machining.
Based directly in Donghai County—China's primary crystal and quartz processing hub—we hold direct, uninterrupted stock of high-purity natural silica sand, plasma-fused ingots, and oversized mother cylinders. By circumventing European third-party distribution markups, UK buyers realize 35% to 55% procurement savings while securing stable, 12-month fixed-price contracts.
UK engineering incubators in Oxford, Cambridge, and Bristol frequently require iterative customized quartz rings for novel reactor designs. Our tooling-free CNC ultrasonic machineries allow rapid turnaround from 3D CAD (STEP/DWG) models to physical, cleanroom-bagged prototypes within 5 to 7 operational days, shipped via direct air freight to Heathrow or Manchester.
Every quartz ring engineered for British destinations conforms strictly with UKCA, REACH, and RoHS regulatory frameworks. Our factory executes 100% helium mass-spectrometry leak detection on flanged ring joints, non-destructive optical polarization stress analysis, and vacuum cleanroom double-PE shrink wrapping to guarantee immediate fab insertion upon arrival.
Proven engineering architectures optimized for process yields, prolonged maintenance cycles, and severe vacuum environments.
Deployed in Inductively Coupled Plasma (ICP) and Reactive Ion Etching (RIE) systems. Our ultra-dense fused silica rings ensure uniform plasma sheath boundary distribution across compound semiconductor substrates, preventing edge roll-off.
For horizontal and vertical furnace tubes operating across Sheffield, Birmingham, and Newcastle manufacturing facilities. Precision ground bevels and mating quartz sealing rings guarantee leak rates below 1×10⁻⁹ mbar·l/s at 1100°C.
Compound semiconductor foundries synthesizing GaN and SiC on silicon rely on our thermal-barrier quartz retainer rings to maintain temperature uniformity across rotating planetary graphite susceptors.
Designed for synchrotrons (such as Diamond Light Source in Oxfordshire) and advanced aerospace test chambers. Flame-polished optical finish ensures optical transmission exceeding 92% across the 260nm to 2200nm spectrum.
Heavy-duty dielectric quartz spacer rings engineered for commercial sputtering and magnetron plasma deposition coaters in the UK glass, window, and architectural solar panels sectors.
Supporting leading academic departments (Imperial College London, Manchester, Cambridge, Oxford) with low-volume, high-complexity quartz rings for cutting-edge materials and quantum physics exploration.
Clear answers addressing import tariffs, technical certifications, chemical etching life cycles, and packaging standards.
For standard CNC cut and ground rings, fabrication takes 7 to 10 working days. Rapid prototyping can be expedited to 5 days. We partner with DHL Express, FedEx Priority, and air cargo forwarders delivering DDP (Delivered Duty Paid) to British facilities within 3 to 5 business days after customs clearance at London Heathrow or East Midlands hubs.
Plasma erosion rate in dry etching is directly proportional to hydroxyl (OH) content and internal bubble micro-inclusions. We utilize low-OH synthetic quartz or high-purity electrical fused quartz with bubble class 0 (DIN 58927), decreasing the chemical sputter etching rate by up to 30% compared to standard industrial glass.
We accept native 3D files (STEP, IGES, SolidWorks) and 2D mechanical schematics (AutoCAD DWG, DXF, or vector PDF). We routinely hold external/internal diameter tolerances of ±0.01mm, with high-precision critical surfaces reaching ±0.005mm, concentricity within 0.008mm, and flatness below 0.003mm.
Following final ultrasonic multi-stage acid cleaning (HF etching and 18.2 MΩ·cm DI water cascade rinsing), parts are dried under Class 100 HEPA air hoods. They are vacuum sealed in medical-grade double-layer antistatic polyethylene (PE) bags, secured within custom pre-molded EVA shock-absorbing foam, and packaged in heavy export-grade plywood crates.
Yes. Our CNC ultrasonic cutting platforms accommodate single-piece outer diameters up to 850mm and wall thicknesses from 1.0mm up to 80mm. We fabricate focus rings and process kit shields compatible with 150mm, 200mm, and 300mm wafer processing systems across Lam, Applied Materials, and TEL tool configurations.
Every shipment includes a full Quality Assurance Dossier: Glow Discharge Mass Spectrometry (GD-MS) purity breakdown certifying SiO₂ > 99.998%, 3D CMM dimensional inspection protocols, surface roughness profile traces, and Certificate of Conformity (CoC) matching your purchase order requirements.
Discover our comprehensive range of high-temperature furnace tubes, oversized vacuum vessels, optical plates, and drawing-specific quartzware for UK advanced engineering.
Eliminate lead time bottlenecks and protect process yields. Connect directly with our Donghai technical engineering center for non-disclosure agreements (NDAs), drawing assessments, and cost benchmarking.