Direct factory-engineered quartz tubes, diffusion carriers, and thermal insulation solutions tailored for sub-micron silicon fabrication lines and demanding thermal process atmospheres.
Deconstructing the crystalline lattice kinetics, elemental stoichiometry, and thermodynamic limits governing modern industrial quartz manufacturing.
In modern industrial fabrication, the terminology surrounding fused quartz and fused silica represents distinct material synthesis pathways, each dictating specific thermal, dielectric, and optical transmission properties. Fused quartz is synthesized by electro-fusion or oxy-hydrogen gas fusion of high-purity natural silica sand (SiO₂), yielding an amorphous network characterized by exceptional mechanical strength, a high annealing point (~1,140 °C), and minimal bubble density. Conversely, synthetic fused silica is created via the chemical vapor deposition (CVD) or flame hydrolysis of silicon tetrachloride (SiCl₄), yielding sub-ppb trace metal levels virtually free of aluminum, titanium, and alkali ions, albeit typically containing higher hydroxyl ([OH⁻]) concentrations.
For semiconductor diffusion, low-pressure chemical vapor deposition (LPCVD), and rapid thermal processing (RTP), natural fused quartz remains the indispensable carrier. The mechanical rigidity and resistance to sag at operating temperatures between 1,000 °C and 1,250 °C make large-diameter quartz tubes and wafer boats structurally unmatched by alternate ceramics or conventional glasses.
| Material Parameter | Electric Fused Quartz (Type I) | Gas-Fused Quartz (Type II) | Synthetic Fused Silica (Type III) | Testing Standard |
|---|---|---|---|---|
| SiO₂ Purity (%) | ≥ 99.995% | ≥ 99.99% | ≥ 99.9999% | ICP-MS / GDMS |
| Hydroxyl [OH⁻] Content | < 5 – 20 ppm | 150 – 200 ppm | 800 – 1200 ppm (Standard) | FTIR Spectrophotometry |
| Strain Point | 1,075 °C | 1,020 °C | 990 – 1,010 °C | ASTM C598 |
| Annealing Point | 1,180 °C | 1,140 °C | 1,100 °C | ASTM C336 |
| Softening Point | 1,683 °C | 1,660 °C | 1,585 °C | ASTM C338 |
| Thermal Expansion (0–300 °C) | 5.5 × 10⁻⁷ /°C | 5.5 × 10⁻⁷ /°C | 5.2 × 10⁻⁷ /°C | Dilatometry (DIN 51045) |
| Dielectric Constant (1 MHz) | 3.78 | 3.80 | 3.75 | ASTM D150 |
Unlocking vertical integration from raw crystal refining and rotary plasma arc ingot casting to CNC cold machining and micro-flame torch assembly.
Situated in Donghai County (Jiangsu Province), the hub processes over 70% of China's quartz supply. Concentrated refining facilities provide immediate access to purified quartz powder, raw ingots, continuous-draw tubing lines, and specialized gas delivery infrastructures, compressing raw-material procurement lead times by up to 65% compared to decentralized western suppliers.
China's quartz processing lines deploy high-precision 5-axis ultrasonic CNC milling centers paired with proprietary computer-guided glass lathes. Custom quartz boats, multi-slot cassettes, and specialized CVD flanges bypass high mold charges, allowing rapid single-piece prototyping and production ramp-up with tight economic feasibility.
From initial electric two-step fusion to high-temperature hydrogen-oxygen flame welding, multi-stage acid pickling (hydrofluoric-nitric bath), ultra-pure water ultrasonic rinsing, and cleanroom vacuum packaging, the localized supply chain enforces unbroken traceability and ISO 9001 process control.
Navigating stringent international regulatory frameworks, SEMI process standards, cleanroom bagging protocols, and cross-border transit integrity.
Compliance with SEMI C1 (analytical reagent grade purity), SEMI F19 (gas distribution integrity), and ASTM C693 for density verification guarantees that quartz components introduce no mobile ion contamination (Na, K, Li) into active wafer channels.
Following final acid etch and deionized water rinsing (>18.2 MΩ·cm), all precision quartzware undergoes multi-stage vacuum double-bagging inside certified Class 1000 (ISO Class 6) or Class 100 cleanrooms using anti-static, non-outgassing polyethylene films.
Diffusion tubes, oversized quartz reactors, and multi-port bubblers are non-destructively leak-checked using Leybold/Pfeiffer vacuum leak testing stations, certifying leak tightness below 1×10⁻⁸ mbar·L/s to prevent explosive reaction between silane (SiH₄) and ambient oxygen.
Comprehensive third-party ICP-MS testing certificates affirm complete compliance with EU RoHS Directive 2011/65/EU, REACH EC 1907/2006 (SVHC substance lists), and responsible minerals sourcing documentation for cross-border customs clearance without delays.
To satisfy Tier-1 semiconductor wafer fabs and national laboratory procurement bodies, modern Chinese factories operate rigorous six-stage verification regimes. Every manufactured run is supported by raw material mill certificates tracking trace metallic element parts-per-billion (ppb) concentrations for 14 major contaminant elements: Fe, Cu, Ni, Cr, Mn, Co, Na, K, Li, Ca, Mg, Ti, Al, and B.
Coordinate Measuring Machines (CMM) and non-contact laser optical micrometers document dimensional runout, wall thickness uniformity, camber tolerances (< 0.5 mm/m for continuous furnace tubes), and mechanical slot pitch tolerances within ±0.03 mm for wafer-holding quartz boats.
Analyzing thermal, chemical, and physical stress environments across high-yield semiconductor lines, solar cell processing, optical instrumentation, and chemical reactors.
Operational Parameters: 850 °C to 1,200 °C in oxidizing (O₂), wet-oxygen (pyrogenic steam), or inert (N₂, Ar) atmospheres.
Demands: Absolute absence of alkali mobile ions (Na⁺, K⁺) that drift through SiO₂ gate dielectrics causing transistor threshold voltage shifts. Oversized horizontal and vertical furnace tubes must display near-zero thermal creep and sagging over 3,000+ thermal hours.
Failure Prevention: Scheduled thermal cycling ramp rates (< 5–10 °C/min between 600 °C and 1,000 °C) mitigate micro-cracking at welded joints.
Operational Parameters: Boron trichloride (BCl₃) and phosphorus oxychloride (POCl₃) diffusion at 900–1,050 °C.
Demands: Massive volume, large-bore (OD > 350–500 mm) quartz furnace tubes capable of handling large wafer loads with minimal downtime. High chemical inertness against aggressive chlorine and halogen by-products.
Failure Prevention: Periodic acid etching must strictly limit bath concentration to avoid surface pitting that accelerates localized devitrification into high-stress cristobalite crystallites.
Operational Parameters: Continuous ultraviolet and visible light transmission down to 180 nm wavelengths under ambient or pressurized liquid flow.
Demands: Optically homogeneous quartz flow cells, cuvettes, and microchannels featuring bubble-free optical paths (Striae Grade A) and internal surface roughness Ra < 0.2 nm via precision chemical-mechanical polishing (CMP).
Failure Prevention: Elimination of internal residual stresses through precision Lehr annealing cycles eliminates optical birefringence anomalies.
A primary failure mode of fused quartz in high-temperature industrial furnaces is devitrification—the solid-state transformation from the meta-stable amorphous silica glass state into crystalline cristobalite. While fused quartz operates reliably up to 1,150 °C, cristobalite nucleation is rapidly catalysed above 1,000 °C in the presence of trace surface contaminants, specifically alkali metal cations (Na⁺, K⁺, Li⁺) and alkaline earth ions (Ca²⁺, Mg²⁺):
Cristobalite undergoes a displacive β-to-α phase inversion upon cooling through 200 °C to 275 °C, accompanied by a destructive volume contraction of roughly 2.8% to 5.0%. This localized contraction generates extreme tensile shear stress, producing crazing, micro-cracks, and structural failure. Implementing cleanroom-level handling protocols, using lint-free gloves, and avoiding direct epidermal contact prevents catastrophic premature failure in high-temperature industrial service.
How semiconductor scaling, high-power EUV lithography optics, and green energy revolutions are redefining high-purity quartz manufacturing boundaries.
As semiconductor fabs optimize wafer edge-yields and high-capacity PV lines transition to large-format rectangular wafers (G12 format), the demand for continuous fused quartz tubes exceeding 450 mm inner diameter with wall thicknesses of 8.0–12.0 mm has surged. Maintaining geometric circularity and wall thickness tolerances within ±0.3 mm demands AI-driven continuous draw stabilization and computerized thermal profiling.
To support Advanced Packaging, SiC/GaN wide-bandgap epi-wafer fabrication, and EUV mask blanks, conventional oxy-hydrogen fusion is increasingly supplemented by electric arc and radio-frequency (RF) plasma rotary fusion. Plasma-synthesized ingots reduce total metallic impurity content below 1 ppb while yielding zero bubble inclusion (DIN 58927 Class 0), eliminating light refraction and thermal pinholes.
Automated optical inspection (AOI) systems utilizing multi-angle telecentric imaging and laser light scattering now inspect quartz tubes and bell jars at microscopic resolutions. Real-time neural networks classify internal bubble clusters, micro-inclusions, surface scratches, and geometric deviations before shipment, establishing digital component birth certificates.
Direct engineering answers addressing critical design limits, cleaning chemistries, shipping protocols, and custom manufacturing parameters.
To ensure a precise engineering review and avoid tolerance conflicts, custom component RFQs should supply a 2D drawing (PDF/DWG) and 3D CAD model (STEP format) specifying: exact outer diameter (OD), inner diameter (ID), wall thickness, overall length, concentricity/ovality tolerances, and surface finish (clear flame-polished, fine ground, or sandblasted opaque). Furthermore, specify working temperature, process gas chemistry (e.g., presence of HF, HCl, BCl₃), flanged connections (ground ball/socket joints, ISO-KF, ConFlat, or O-ring grooves), and required purity level (4N natural fused quartz vs 5N/6N synthetic silica).
Fused quartz exhibits extraordinary chemical inertness across virtually all acidic and neutral media, including hot nitric acid (HNO₃), sulfuric acid (H₂SO₄), and hydrochloric acid (HCl). The critical exceptions are hydrofluoric acid (HF) and concentrated phosphoric acid (H₃PO₄) above 150 °C, both of which dissolve silica via hexafluorosilicate complexation: SiO₂ + 6HF → H₂SiF₆ + 2H₂O. Quartz is also attacked by strong alkali hydroxide solutions (KOH, NaOH) at elevated temperatures, leading to chemical etching and surface crystallization.
High-purity transparent fused quartz typically supports continuous operation at temperatures up to 1,100 °C (1,373 K) in neutral or oxidizing atmospheres. Intermittent, short-duration thermal excursions can reach 1,250 °C to 1,300 °C without structural deformation. The transformation point (strain point) occurs at approximately 1,075 °C, while softening begins near 1,683 °C. Operating above 1,150 °C requires proper support tooling to prevent sag under structural loads, especially for oversized tubes with high diameter-to-wall-thickness ratios.
Due to the extremely low coefficient of thermal expansion (5.5 × 10⁻⁷ /K), fused quartz possesses exceptional thermal shock resistance and can theoretically withstand cold water quenching from 1,000 °C. However, heavy manual flame welding introduces intense localized thermal stress gradients between the molten weld seam and cooler adjacent areas. Specialized factories utilize computerized multi-point hydrogen-oxygen annealing torches and place assembled units into high-temperature Lehr annealing ovens at 1,140–1,180 °C, slowly ramping down to 900 °C to eliminate residual mechanical stresses.
Exported quartz components are protected through layered cushioning systems designed to absorb vibrational and shock harmonics. Primary packaging entails double-sealed anti-static cleanroom PE bags under vacuum. The sealed items are cushioned within customized high-density polyethylene (EPE) or polyurethane foam shells molded to the exact component profile. Secondary encasement uses reinforced, fumigated plywood export crates fitted with external ShockWatch and Tip-N-Tell impact indicators to monitor dynamic loads during sea and air transit.
Transparent fused quartz is completely melted to eliminate micro-bubbles, achieving optical clarity across UV, visible, and near-IR spectrums with high transmission (>90% at 200–2,500 nm). Opaque or translucent quartz is produced by sintering high-purity quartz sand with controlled micro-porosity (tiny enclosed gas bubbles). These micro-voids scatter radiation, creating a thermal insulation barrier that reflects infrared radiation. Translucent quartz is commonly utilized for thermal baffles, furnace flanges, radiant heat shields, and furnace end-caps.
Explore high-temperature structural insulation rings, precision-ground solid silica rods, and customized reactor chambers built for global semiconductor and laboratory operations.
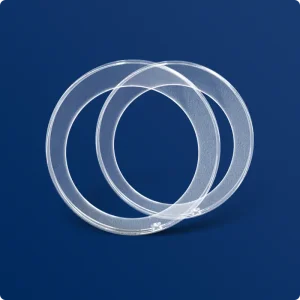
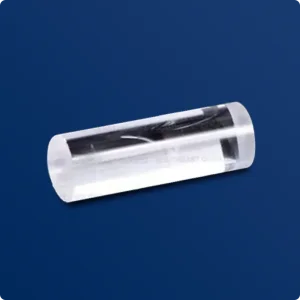
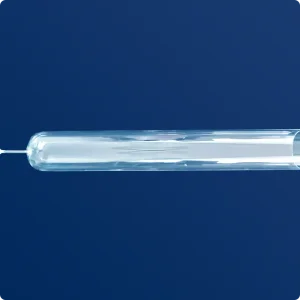
Ensure frictionless supplier alignment by standardizing RFQ data packages across engineering and logistics divisions.
Confirm purity tier (4N 99.99% for standard PV/furnaces vs 5N 99.999% for advanced sub-14nm wafer diffusion) and define [OH⁻] hydroxyl thresholds below 20 ppm to prevent high-temperature sagging.
Detail outer/inner diameter tolerances (typically ±0.15 mm to ±0.5 mm depending on diameter), wall thickness concentricity, camber runout (< 0.5 mm per meter), and face squareness.
Require factory mill test certificates (ICP-MS report), coordinate measuring machine (CMM) dimensional logs, helium leak testing verification, and Class 100/1000 cleanroom packaging.
Mandate custom-molded EPE foam cradles, vapor-barrier inner barrier bags, impact-shock telemetry sensors, and certified fumigated plywood crates for high-value transoceanic transit.