Direct-factory fabrication adhering to ISO 9001 and SEMI standards with complete ICP-MS purity tracking.
How atomic-level purity, laser micro-machining, and next-generation thermal processing redefine the competitive landscape in ultra-high vacuum and high-temperature wafer batching.
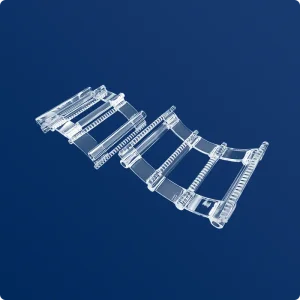
Modern semiconductor architectures such as gate-all-around (GAA) nanosheets and 3D NAND vertical memory stacks demand wafer pitch spacing accurate to within ±0.03 mm. Quartz slotted tubes now leverage automated diamond blade grinding and 5-axis CNC laser ablative technologies to prevent structural micro-fractures, mitigating micro-particle shedding in Class 10/100 cleanrooms.
Thermal stability at 1,150°C–1,280°C relies directly on inhibiting crystallization (cristobalite formation). Premium manufacturers deploy natural rock quartz refined through advanced acid leaching and plasma fusion, bringing total metallic impurities (Al, Fe, Ti, Ca, Mg, Na, K, Li) to strictly under 15 ppm, with specific alkali metals kept beneath 0.5 ppm.
The photovoltaic transition to N-type TOPCon, HJT, and tandem cells demands ultra-large diameter quartz slotted furnace tubes capable of handling oversized wafers (M10, G12). These structural components withstand continuous boron or phosphorus diffusion at high temperatures without sagging, utilizing wall-thickness optimizations of 6.0 mm to 9.5 mm.
In high-throughput fabrication facilities, quartz components are high-risk process consumables. A single structural failure or particle release event incurs millions in contaminated batch losses.
Procurement directors in Europe, the Americas, and Southeast Asia look beyond unit price to evaluate full lifecycle yield impact. Key technical requirements include:
Global semiconductor fab expansions have created acute demand for localized raw stock reserves and rapid CNC tooling customization. Factory partners must deliver:
| Performance Parameter | Commercial Grade Quartz | High-Purity Semiconductor Grade | Synthetic Fused Silica Grade |
|---|---|---|---|
| Total Metallic Impurities | < 35 ppm | < 15 ppm (Typical < 8 ppm) | < 0.1 ppm |
| Devitrification Inception (Air) | ~1,050°C | ~1,180°C – 1,220°C | > 1,300°C |
| Hydroxyl (OH⁻) Content | 120 – 180 ppm | < 30 ppm (Dry < 5 ppm) | < 1 ppm or > 1000 ppm (Opt.) |
| Dimensional Tolerance (Slots) | ±0.15 mm | ±0.03 mm to ±0.05 mm | ±0.01 mm |
| Primary Target Application | General Laboratory & Lighting | LPCVD, Oxidation, Diffusion | Sub-7nm Lithography, Extreme Plasma |
Holistic engineering that links quartz vessel geometry with fluid thermodynamics, gas dispersion dynamics, and automated robotic wafer handling.
At working temperatures hovering at 1,100°C for hours, thermal sagging causes uneven gas boundary layers. Our thickened base quartz slotted configurations maintain bore straightness over extended campaigns, delivering uniform oxide growth across every wafer.
LPCVD processes coat furnace walls with high-stress films that can crack ordinary quartz tubes during cool-down. We apply proprietary internal surface modifications and precision annealing to balance thermal expansion mismatch stresses, tripling maintenance cycles.
Gallium Nitride (GaN) and Silicon Carbide (SiC) epitaxy demand corrosion resistance against halogen gases (HCl, Cl₂) and ammonia (NH₃). Our ultra-dense, bubble-free fused quartz tubes prevent sub-surface bubble expansion and micro-pitting under corrosive gases.
From cleanroom ultrasonic cleaning to custom shock-absorbent overseas shipping containers, our quality system leaves zero room for transit or contamination defects.
Every slotted tube assembly with welded flanges, ball joints, or gas inlets passes vacuum testing using helium mass-spectrometry down to <1×10⁻⁹ mbar·L/s, verifying air-tight performance under high-vacuum LPCVD and hazardous hydride flows.
Parts undergo electronic-grade HF and HNO₃ immersion etching to strip micro-particulate swarf, followed by 18.2 MΩ·cm deionized water cascade rinsing and Class 100 HEPA air drying before vacuum-sealed multi-layer packaging.
Oversized quartz tubes (often over 2 meters long) travel in tailored suspended-foam flight crates fitted with 3-axis drop indicators and tilt sensors, maintaining safe delivery to destinations across Europe, North America, and Asia.
Anticipating next-generation node requirements through continuous R&D across high-purity synthetic quartz, plasma torch flame stabilization, and automated metrology.
Traditional mechanical diamond wheel slotting can leave sub-surface micro-checks that trigger devitrification nuclei at elevated temperatures. Our roadmap deploys picosecond UV laser cutting in liquid environments. This approach delivers zero heat-affected zone (HAZ), eliminates mechanical micro-cracks, and maintains slot tolerances within ±0.01 mm.
To resist higher thermal cycles (>1,300°C) without physical sagging, development centers on refractory metal doping (such as rare-earth aluminosilicate stabilization) within the vitreous silica network. This advances viscosity-temperature profiles, boosting annealing points by roughly 80°C to 110°C over natural quartz.
Clear, direct technical answers for fab engineers, manufacturing directors, and purchasing teams.
Devitrification is the phase transformation of amorphous vitreous silica into crystalline cristobalite. It generally starts above 1,150°C and accelerates in the presence of surface contaminants, notably alkali metals (sodium, potassium, lithium) and alkaline earths (calcium, magnesium). Even finger oils left during handling act as nucleation centers. At high temperatures, cristobalite develops with a different thermal expansion coefficient, causing micro-cracking and hazing during cooldown. Using high-purity quartz stock (<0.5 ppm alkali), cleaning in cleanroom acid baths, and wearing clean handling gloves significantly delays devitrification.
We use synchronized 5-axis CNC diamond saw assemblies with continuous laser-interferometer position feedback. Machining takes place in temperature-regulated cutting cells with constant chilled deionized water lubrication to eliminate thermal expansion of the workpiece during grinding. Our team checks slot pitch, slot depth, and perpendicularity on a coordinate measuring machine (CMM) to meet tolerances within ±0.03 mm across the full loading bed length.
Yes. We regularly build custom designs directly from standard engineering file formats (STEP, IGES, DWG, DXF, and PDF). Our engineering team reviews the drawing for wall thickness balance, flame-working clearances, and potential thermal concentration areas, returning manufacturability reviews (DFM) within 24 hours.
Standard fused quartz contains between 100 to 200 ppm of hydroxyl radicals (OH⁻), which lowers the material's viscosity and softens the glass network at elevated temperatures. Low-hydroxyl quartz (OH⁻ < 5 to 30 ppm) raises the strain point and annealing point by 50°C to 80°C. For continuous operations between 1,150°C and 1,250°C, low-OH quartz tubes offer substantially greater resistance to structural sagging and oval deformation, extending service life by 40% to 75% depending on internal thermal profiles.
Every delivery includes a standard quality assurance packet containing: (1) An ICP-MS chemical impurity analysis report verifying trace metal concentrations; (2) A CMM dimensional inspection certificate matching the approved engineering print; (3) A helium mass-spectrometry leak test report for welded or flanged joints; and (4) Material certificates confirming the silica stock grade.
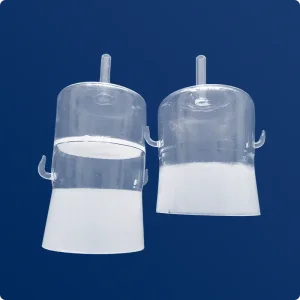
Complementary precision quartzware manufactured to the same tight quality standards as our slotted diffusion tubes.
Send your 2D/3D component drawings, thermal cycle parameters, and wafer pitch specifications. Our engineering team reviews manufacturability and returns a quotation within 24 hours.