Standardized, ISO 9001:2015-certified fused quartzware manufactured via thermal plasma electric fusion and continuous drawing for POCl3 diffusion, LPCVD, thermal oxidation, and semiconductor-grade annealing.
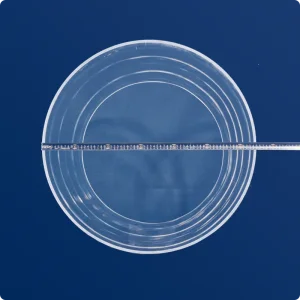
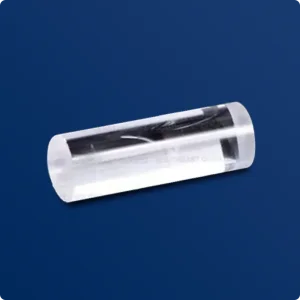
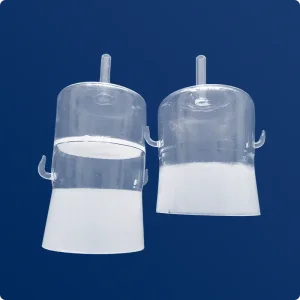
Analyzing the macro-shift from P-Type PERC cells to N-Type TOPCon, HJT, and Perovskite Tandem Architectures, and the resulting thermal stress thresholds imposed on fused silica chambers.
The global renewable energy landscape is witnessing a generational manufacturing pivot. Over the past five years, the crystalline silicon photovoltaic (PV) industry has completed a monumental transition away from legacy P-type Passivated Emitter and Rear Cell (PERC) technology toward high-efficiency N-type solar cells, dominated by Tunnel Oxide Passivated Contact (TOPCon) and Heterojunction (HJT) architectures. This technological leap has revolutionized process chemistry within cell manufacturing plants worldwide. Where legacy diffusion operations previously tolerated continuous operating temperatures between 850°C and 900°C, modern N-type TOPCon POCl3 liquid source diffusion, LPCVD tunneling oxide growth, and Boron tri-bromide (BBr3) diffusion routinely demand sustained thermal operational ranges of 1,150°C to 1,280°C.
In this hyper-demanding thermal ecosystem, the solar quartz furnace tube is no longer a passive vessel—it is a critical process boundary whose material purity, structural geometry, and thermodynamic resistance directly dictate wafer conversion efficiency, minority carrier lifetime, and fab yield. With photovoltaic wafers scaling aggressively from M6 (166 mm) to M10 (182 mm), G12 (210 mm), and rectangular G12R standards, quartz reaction chambers have correspondingly expanded in outer diameter (OD) from Ø280 mm to Ø450 mm, Ø520 mm, and exceeding Ø600 mm, with overall lengths spanning between 2,800 mm and 4,500 mm. At these gargantuan dimensions, maintaining dimensional stability under severe gravitational sagging moments and preventing catastrophic devitrification require state-of-the-art fused silica synthesis and advanced manufacturing controls.
Total metallic impurities suppressed below 15 ppm, preventing transition metal lattice poisoning.
Engineered for long-cycle TOPCon Boron & POCl3 diffusion without structural collapse.
Minimizes high-temperature structural viscosity breakdown and retards cristobalite growth.
Ensures automated AGV wafer-boat loading arms insert smoothly without mechanical collision.
Fused silica in its pristine state is a thermodynamically metastable glass. When continuously exposed to solar cell diffusion furnace regimes exceeding 1,100°C, the amorphous SiO2 network experiences a driving force toward crystallographic restructuring into beta-cristobalite. This devitrification process begins primarily at surface nucleation sites induced by alkali metal ions (Sodium [Na], Potassium [K], Lithium [Li]) and alkaline earth contaminants (Calcium [Ca], Magnesium [Mg]). Even single-digit parts-per-billion (ppb) surface contamination catalyzes cristobalite crystalline growth fronts. Upon cycle cooling through the 200°C–270°C window, beta-cristobalite abruptly transitions to alpha-cristobalite, accompanied by a sudden 5% volume contraction that causes microscopic micro-cracking, crazing, vacuum compromise, and catastrophic structural failure.
Procurement directors and fab process owners evaluate high-purity quartz furnace tubes on three non-negotiable vectors: chemical impurity limits, structural viscosity at 1,200°C, and dimensional concentricity.
For gigawatt-scale solar cell fabs in Southeast Asia, Europe, North America, and mainland China, an unexpected quartz tube failure equates to tens of thousands of dollars in lost throughput, scrap wafers, and thermal furnace recalibration downtime. Consequently, international procurement teams have established strict incoming acceptance criteria. Trace transition metals such as Iron (Fe), Copper (Cu), and Nickel (Ni) must be constrained to ultra-trace thresholds, as volatile gaseous metal halides easily diffuse through the furnace atmosphere during chlorination and wet oxidation, causing deep-level recombination defects within the crystalline silicon p-n junctions.
| Element / Physical Parameter | Standard PV Grade Tube | Advanced N-Type TOPCon Grade | Semiconductor Ultra-Pure Grade | Analytical Metrology Protocol |
|---|---|---|---|---|
| Silicon Dioxide (SiO2) Purity | ≥ 99.99% | ≥ 99.998% | ≥ 99.9995% | Difference Gravimetric Calculation |
| Hydroxyl Radical ([OH-] Content) | ≤ 30 ppm | ≤ 15 ppm | ≤ 5 ppm (Vacuum Baked) | FTIR Spectrophotometry (2.73 μm) |
| Alkali Metals (Na + K + Li) | ≤ 1.8 ppm | ≤ 0.6 ppm | ≤ 0.15 ppm | ICP-MS (Inductively Coupled Plasma) |
| Transition Metals (Fe + Cu + Ni + Cr) | ≤ 1.2 ppm | ≤ 0.35 ppm | ≤ 0.08 ppm | ICP-OES / High-Resolution ICP-MS |
| Softening Point (log η = 7.6) | 1,665 °C | 1,683 °C | 1,710 °C | ASTM C338 Fiber Elongation |
| Annealing Point (log η = 13.0) | 1,180 °C | 1,215 °C | 1,230 °C | ASTM C336 Beam Bending Viscometer |
| Outer Diameter (OD) Tolerance | ± 1.5 mm | ± 0.8 mm | ± 0.4 mm | Multi-Axis Laser Micrometer Gauging |
| Wall Thickness Uniformity | ± 10% | ± 6% | ± 3% | Ultrasonic Pulse-Echo Transducer |
| Helium Leak Test Rate | ≤ 1.0 × 10⁻⁷ mbar·l/s | ≤ 1.0 × 10⁻⁹ mbar·l/s | ≤ 2.0 × 10⁻¹⁰ mbar·l/s | He Mass Spectrometry Leak Detection |
How advanced flame lathe welding, automated fire-polishing, and controlled dehydroxylation double the operational lifespan of solar diffusion tubes.
Oversized tubes (>Ø450mm) spanning 3+ meters in horizontal diffusion systems experience substantial bending moments. We employ computer-controlled electric fusing that ensures uniform radial wall thicknesses of 6.0 mm to 9.5 mm, minimizing differential hoop stresses and reducing creep deformation under prolonged 1,200°C thermal exposure.
High hydroxyl concentrations act as lattice terminators, breaking the continuous silicon-oxygen tetrahedron network and drastically lowering viscosity at elevated temperatures. Our factory integrates secondary ultra-high vacuum baking furnaces at 1,150°C, stripping OH- contents below 15 ppm to deliver exceptional structural stiffness.
Micro-notches, micro-cracks, and saw cutting marks serve as catastrophic stress risers during thermal cycling. All tube ends, custom flanges, ball joints, and gas injection capillaries are treated with automated oxy-hydrogen torches to achieve a mirror-smooth flame polish, sealing surface lattice bonds and extending thermal fatigue life.
To eliminate vacuum leakage and process gas poisoning during critical LPCVD Poly-Silicon deposition and BBr3 diffusion, 100% of our flanged and closed-end quartz tubes undergo multi-point helium mass spectrometry leak testing, guaranteeing vacuum integrity down to 1.0 × 10⁻⁹ mbar·l/s.
From Donghai County—the silicon capital of China—to cleanroom manufacturing bays across Europe, Asia, and the Americas.
A resilient semiconductor and solar cell equipment supply chain relies on unwavering transparency. Located in Donghai County, Jiangsu Province, Lianyungang Southeast Quartz operates in close geographical alignment with China's largest natural crystal and high-purity silica raw material deposits. This direct supply proximity safeguards our plant from global raw material bottlenecks and offers uncompromised batch-to-batch traceability from refined granular quartz sand to finished hot-worked chambers.
Every batch of quartz furnace tubes, wafer boats, quartz rings, and custom manifolds is backed by rigorous third-party and internal documentation:
Anticipating the requirements of 240mm+ ultra-large wafers, high-aspect-ratio tandem cells, and synthetic inner-liner coatings.
Developing continuous high-draw electric fusion towers capable of producing furnace tubes exceeding Ø650 mm with wall thickness tolerances constrained within ±0.3 mm for next-gen clustered diffusion boats.
Applying chemical vapor deposition (PCVD) synthetic amorphous silica inner liners onto natural fused quartz substrates, achieving <1 ppb trace purity at the reaction interface while maintaining structural thermal sag resistance.
Deploying six-axis multi-head robotic welding torches to eliminate manual hand-flame variability, ensuring 100% repeatability on complicated quartz bubblers, injectors, and flanged manifold terminations.
Integrating optical coherence tomography (OCT) and AI machine vision to scan internal fused quartz wall structures for micro-bubbles, crystalline inclusions, and striae down to 10-micron resolutions.
Detailed technical responses on devitrification prevention, dimension customization, lifetime expectancy, and installation handling.
Expanding your high-temperature process suite with CNC-machined quartz rings, heating lamp holders, custom thermal plates, and diffusion carrier accessories.
Submit your custom quartz tube, boat, or chamber drawings (PDF / DWG / STEP). Our senior quartz application engineers provide full manufacturability audits, finite element thermal deformation analyses, and competitive factory-direct quotations within 24 hours.