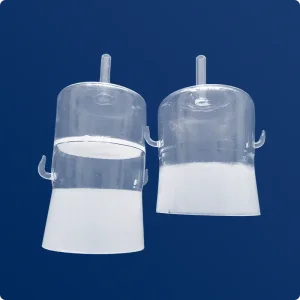
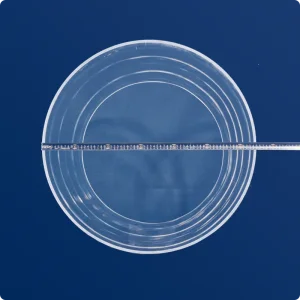
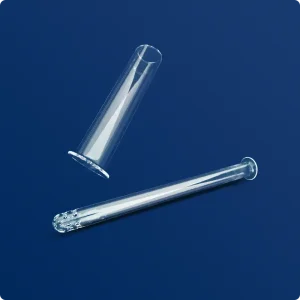
Explore our high-performance fused quartz rods, furnace tubes, wafer carriers, and custom machined quartzware manufactured to rigid international DIN/ISO quality metrics with complete lot traceability.
Modern electronic and optical industries rely on high-purity fused quartz rods (SiO₂ ≥ 99.99%) for structural integrity under extreme heat, chemical inertness against harsh etchants, and broadband optical transmittance. The process of slicing, profiling, and finishing solid quartz rods into microscopic pins, spacer rods, optical light guides, and furnace structural members represents a pivotal link in global advanced manufacturing.
In ultra-clean fab environments, wafer cassettes, lifter pins, push rods, and wafer paddle fixtures must withstand process temperatures up to 1,200 °C without trace metal outgassing. Precise rod cutting ensures zero dimensional drift under thermal cyclings during low-pressure chemical vapor deposition (LPCVD) and wet chemical etch passes.
Cut fused silica rods function as precision cladding, end-caps for high-power fiber lasers, and light conduits. End-face cutting accuracy, perpendicularity within 0.05°, and optical-grade flame or chemical mechanical planarization (CMP) prevent scatter losses in telecommunications and solid-state industrial laser systems.
From TOPCon and HJT solar wafer diffusion tubes to infrared emitter supports, segmented quartz rods act as heat-resistant supports and electrode feedthrough isolators. Their coefficient of thermal expansion (5.5 × 10⁻⁷ /°C) guarantees zero failure under radical shock cycles up to 1,150 °C.
Cutting vitreous silica demands specialized cold machining and thermal cleavage processes. Vitreous silica has extreme hardness (Mohs 7) combined with fracture brittleness. Incorrect slicing introduces micro-cracks, edge chipping, and latent mechanical stress that lead to catastrophic shatter at operating furnace temperatures.
Utilizing electroplated diamond endless wires running at 40-60 m/s with micro-miter tension control, this method reduces kerf loss to less than 0.25 mm. It achieves high parallelism (≤ 0.02 mm) across rod bundles with near-zero micro-crack propagation, ideal for high-volume semiconductor pin manufacturing.
Equipped with synthetic resin and metal-bonded diamond tools, our 5-axis CNC machines perform chamfering, center-drilling, keyway slotting, and thread cutting directly onto rod segments. Flood-cooling systems using treated deionized fluid prevent local thermal shock during aggressive tooling paths.
For heavy-diameter rods (OD 40 mm – 150 mm), controlled thermal laser or oxy-hydrogen scoring induces a clean tensile fracture. Automated post-cut fire polishing melts sharp perimeter fractures, raising mechanical flexural strength from 50 MPa to over 80 MPa while restoring optical surface transparency.
Subsurface micro-cracks created during mechanical sawing act as stress concentrators during high-temperature cycling. Southeast Quartz applies a multi-stage post-cut chemical acid etching process (HF/HNO₃ blend) to etch away 15–30 μm of damaged boundary layer, followed by a 1,150 °C annealing soak to eliminate internal strain before final dimensional validation.
China produces more than 70% of the world's commercial fused quartz products. Located in Donghai County, Jiangsu Province—recognized worldwide as the primary hub of quartz refining and fabrication—Lianyungang Southeast Quartz Products Co., Ltd. capitalizes on unique structural supply-chain advantages that deliver exceptional value to international buyers.
Direct proximity to top-tier fused silica refining facilities gives Southeast Quartz guaranteed access to premium transparent, opaque, and synthetic quartz ingots without inland transit delays.
Our facility operates high-throughput diamond cutting saws and specialized CNC profiling centers simultaneously. Rapid fixture custom tooling allows 48-hour turnarounds on initial prototypes.
Every batch goes through dimensional optical profile projection, CMM inspection, helium mass-spectrometry leak detection, and ICP-OES trace element impurity verification.
Cleanroom vacuum poly-bagging, shock-absorbent wooden crating, and optimized export paperwork through Lianyungang/Shanghai ports ensure zero damage and seamless customs clearance worldwide.
Compare our typical engineering parameters across different grades of fused silica and transparent fused quartz rods. Tailored tolerances, custom diameters (OD 1 mm to 200 mm), and specific end-finishes are supplied according to customer CAD/STEP files.
| Property Parameter | Semiconductor Grade (SG-01) | Optical / Laser Grade (OG-02) | Industrial Heating Grade (HG-03) | Verification Method |
|---|---|---|---|---|
| SiO₂ Purity Level | ≥ 99.998% (4N8) | ≥ 99.999% (5N) | ≥ 99.99% (4N) | ICP-MS / ICP-OES |
| Hydroxyl (OH⁻) Content | < 5 ppm (Low-OH) / ~30 ppm | < 1 ppm (Dry Synthetic) / 200 ppm | < 30 ppm | FTIR Spectrophotometry |
| Diameter Range (OD) | Ø 1.0 mm – 120.0 mm | Ø 2.0 mm – 80.0 mm | Ø 3.0 mm – 200.0 mm | Laser Micrometer (Dual Axis) |
| Cutting Length Tolerance | ± 0.02 mm (CNC Sliced) | ± 0.01 mm (Lapped) | ± 0.10 mm (Saw Cut) | Digital Linear Encoder / CMM |
| End-Face Perpendicularity | ≤ 0.05° | ≤ 0.01° (Optically Aligned) | ≤ 0.15° | Optical Autocollimator |
| Surface Roughness (Ra) | Ra 0.1 μm – 0.4 μm (Ground) | Ra < 0.5 nm (Super-Polished) | Ra 0.8 μm – 1.6 μm | White Light Interferometry |
| Max Operating Temperature | 1,150 °C (Continuous) / 1,280 °C | 1,100 °C (Continuous) / 1,250 °C | 1,100 °C (Continuous) / 1,200 °C | Thermal Dilatometry Analysis |
| Thermal Shock Resistance | 1,100 °C to 20 °C Water: No Break | 1,100 °C to 20 °C Water: No Break | 1,000 °C to 20 °C Water: No Break | Quench Cycling Test |
| End-Face Finishes | Chamfered, Acid-Etched, Fire-Polished | Optical Flat (λ/4 to λ/10), AR Coated | Saw-Cut, Ground Bevel, Fire-Sealed | Visual & Surface Profiler |
Driven by technological transitions in next-generation microelectronics, wide-bandgap semiconductors (SiC/GaN), green hydrogen, and aerospace photonics, the procurement criteria for precision-cut quartz rods have advanced substantially.
Leading 3nm and 2nm fabs demand quartz components with near-zero heavy metal contamination (Fe < 0.05 ppm, Cu < 0.01 ppm, Na/K/Li < 0.1 ppm). In furnace support assemblies, alkali elements diffuse into silicon channels, destroying chip yields. Precision-sliced rods must pass stringent cleanroom packaging and hot nitric leaching tests.
Global buyers increasingly specify diamond wire sawing over conventional ID blades. This shift delivers 40% reduction in kerf loss, superior surface parallelism, and shallower subsurface damage, translating into fewer micro-cracks and significantly longer service life in high-vibration plasma etch chambers.
Procurement teams now minimize vendor tiers by combining quartz raw material sourcing, multi-axis machining, optical end-face polishing, and cleanroom vacuum packaging under a single ISO 9001 certified manufacturer. This eliminates inter-process logistics damage and guarantees end-to-end quality assurance.
Clear, comprehensive answers to technical, operational, and supply chain queries raised by procurement managers, process engineers, and research directors.
Complete your bill of materials with our precision quartz glass rings, customized instruments, oversized process tubes, and furnace structural assemblies. Engineered for maximum thermal cycling endurance and corrosive gas containment.