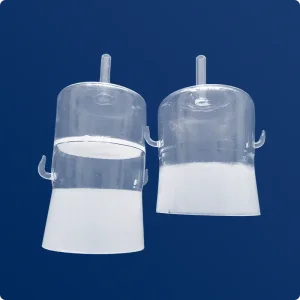
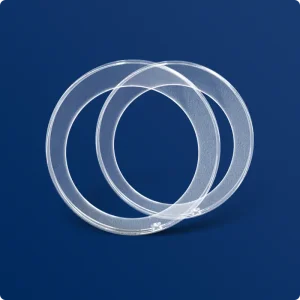
Direct factory supply of fused silica rings, oversized furnace tubes, and custom high-temperature laboratory quartzware manufactured to sub-millimeter tolerances.
A rigorous examination of microcrystalline matrix morphology, mechanical load endurance, and chemical inertness under extreme industrial environments.
In modern industrial design, semiconductor processing, and heavy-duty architectural fabrication, the transition from unrefined natural minerals to high-performance custom artificial quartz stone represents a fundamental leap in materials science. Unlike natural granite or marble, which suffer from inherent geological fissures, micro-porosity, and variable mineral density, artificial quartz surfaces and precision-fused silica matrices are engineered at the molecular and grain level. Utilizing high-purity natural silica sand (≥99.9% SiO₂) bonded with advanced polymeric resin systems or consolidated via plasma-fusion sintering, custom quartz engineered materials offer unprecedented structural uniformity, thermal shock resistance, and zero-stain imperviousness.
As a premier custom artificial quartz stone manufacturer based in Donghai, Jiangsu—the epicentre of China's quartz and silicon materials industrial cluster—our engineering protocols fuse decades of hot-flame metallurgical expertise with high-precision CNC cold-machining. Whether delivering vacuum vibro-compressed slabs for high-traffic commercial spaces or manufacturing monolithic fused quartz furnace tubes capable of sustaining continuous service temperatures up to 1,100 °C, our facility guarantees verifiable physical characteristics backed by comprehensive ASTM, ISO, and CE testing protocols.
Pioneering sustainable composite binders, sub-micron particle optimization, and zero-crystalline silica bio-resins for safe global compliance.
Addressing occupational health mandates such as Safe Work Australia and OSHA standards by formulating advanced sintered stone variants and low-respirable crystalline silica (RCS) minerals, maintaining extreme hardness while eliminating respiratory cutting hazards.
Deploying advanced high-frequency vibration algorithms with 100-ton hydraulic compaction under 20 mbar negative pressure. Real-time sensor telemetry optimizes particle distribution from 0.1 mm to 6 mm, maximizing flexural strength past 55 MPa.
Integrating antimicrobial titanium dioxide (TiO₂) and photo-catalytic self-cleaning top-coats directly into the matrix, enabling surgical-grade hygiene in healthcare surfaces and thermal UV degradation resistance in high-exposure architectural installations.
Discover how custom-formulated artificial quartz stone and fused silica components support demanding commercial, laboratory, and high-tech manufacturing ecosystems.
Non-outgassing surfaces, furnace tubes, and carrier boats resistant to hydrofluoric etching and elevated temperatures. Eliminates trace metallic contamination down to ppb levels inside wafer-processing chambers.
Custom-molded bench surfaces and quartz reaction cells immune to concentrated acids (excluding HF), organic solvents, and thermal shock. Seamless, non-porous slabs simplify decontamination.
Precision-cut custom quartz slabs, countertops, and reception monoliths tailored for luxury hotels, transit hubs, and corporate headquarters requiring zero maintenance and high flexural durability.
High-purity quartz bell jars, diffusion carriers, and thermal baffle plates crucial for continuous N-type monocrystalline silicon ingot pulling and automated photovoltaic cell passivation lines.
Quantitative empirical benchmark data validating custom artificial quartz performance parameters.
| Performance Parameter | Custom Artificial Quartz Stone | Natural Granite | Natural Marble | Solid Surface (Acrylic) | Testing Standard |
|---|---|---|---|---|---|
| Mohs Hardness | 6.5 – 7.0 (High Scratch Resist) | 5.5 – 6.5 (Variable) | 3.0 – 4.0 (Easily Scratched) | 2.5 – 3.0 (Soft) | EN 101 / ASTM C704 |
| Water Absorption Rate | < 0.02% (Non-Porous) | 0.2% – 0.5% (Requires Sealing) | 0.5% – 2.0% (Highly Porous) | 0.05% – 0.1% | ASTM C97 / EN 14617-1 |
| Flexural Strength (Modulus) | 45 – 65 MPa | 12 – 18 MPa | 8 – 14 MPa | 25 – 35 MPa | ASTM C880 / EN 14617-2 |
| Acid & Alkali Resistance | Class A / No Etch (Household/Reagent) | Moderate (Sensitive to acids) | Poor (Immediate acid etching) | Good (Susceptible to acetone) | ASTM C650 / EN 14617-10 |
| Stain Resistance Rating | Class 5 (Highest Protection) | Class 3 (Requires constant seal) | Class 1–2 (Prone to staining) | Class 4 | ANSI Z124.6 / EN 14617-10 |
| Microbial & Bacterial Safety | NSF 51 Food Contact Approved | Pore harbors bacteria | Requires chemical biocide | Hygienic | NSF / ANSI Standard 51 |
Capitalizing on primary resource proximity, automated MES smart plants, and vertically integrated processing clusters.
Sourcing large-scale commercial or high-specification industrial quartz components requires dependable supply chain stability, uncompromised raw ore quality, and rigid batch consistency. Located in Donghai County, Jiangsu, our manufacturing facility sits within the preeminent quartz trading and processing cluster on the Eurasian continent. This strategic positioning provides our factory direct access to premier high-purity crystalline silica sand deposits, plasma-grade quartz ingots, and premium silicon derivatives without intermediary transport bottlenecks or raw material supply interruptions.
Our Industry 4.0 plant deployment combines fully automated powder blending, precise volumetric resin distribution, and supersonic optical grain sorting. Real-time computerized manufacturing execution systems (MES) oversee every slab press cycle and furnace tube pull, logging individual batch cure kinetics, thermal annealing gradient data, and laser-guided wall-thickness profiles. By uniting raw mineral refining, hot flame glass-working, multi-axis cold machining, and helium-leak verification within our own footprint, we dramatically shorten standard international production cycles from 8-12 weeks down to just 14-21 business days.
High-resolution spectroscopic grain grading separates raw quartz by purity, eliminating iron contaminants below 15 ppm.
Continuous vacuum compression under 100-ton hydraulic force prevents air pockets and ensures high density.
Computerized kilns maintain precise 90°C - 110°C polymerization curves, releasing residual monomeric stress.
36-head automated abrasive grinding lines achieve high-gloss, matte, leathered, or custom micro-textures.
Mass-spectrometer vacuum leak inspection and coordinate measuring machines verify strict dimensional tolerances.
A comprehensive technical roadmap designed to streamline requests for quotations (RFQs) for EPC contractors, OEM buyers, and architects.
Submit engineering CAD designs in DXF, DWG, STEP, or PDF formats. Our optical and mechanical engineering group validates manufacturability, draft angles, thermal expansion allowances, and structural edge beveling within 24 hours.
Standard architectural slabs up to 3250 × 1650 mm (thicknesses of 15mm, 20mm, 30mm) alongside oversized custom industrial quartz tubes up to 500 mm OD, with continuous lengths reaching 3000 mm, cut to custom shapes.
Reinforced A-frame timber crates with fumigation heat-treatment certifications (ISPM 15). Individual quartz glass components receive moisture-barrier vacuum polybags, shock-absorbent EPE foam lining, and drop-sensor tags.
Rigorous certifications guarantee unhindered customs clearance, green building credits, and food-safe laboratory approvals.
Certified for direct exposure in commercial kitchen counters, food-processing plants, and splash zones with zero toxic leaching or heavy metal migration.
Ensures ultra-low volatile organic compound (VOC) emissions, contributing points directly to LEED, BREEAM, and WELL certified green architectural buildings.
Certified conformity with European Union modular tile, flooring, and dimensional stone standards, including slip-resistance and freeze-thaw cycle testing.
Full support for safe dry-cutting and wet-processing safety documentation (SDS), keeping partners compliant with evolving regional respirable silica laws.
Targeted insights addressing critical material parameters, manufacturing thresholds, and procurement logistics.
Artificial quartz stone (engineered stone) consists of 90-93% natural crystalline quartz sand consolidated with high-grade polymer resins and color pigments under vacuum vibro-compression, designed primarily for high-wear architectural surfaces. Fused quartz (or fused silica) is a 99.99% pure monolithic silicon dioxide (SiO₂) glass melted at over 1,700 °C, purpose-built for extreme-temperature industrial furnace tubes, semiconductor ware, and optical windows.
Please provide a 2D or 3D technical drawing (PDF, DXF, DWG, or STEP format) outlining major outer/inner dimensions, wall thickness tolerances, edge finishes, and cutouts. Additionally, specifying your thermal operating temperature, working chemical atmosphere, and target batch or container quantities ensures our engineers can verify manufacturability and recommend the optimal material formulation within 24 hours.
In artificial stone production, our vacuum vibro-compression operates under negative pressure (≤20 mbar) to eliminate entrapped air, while computerized multi-zone post-cure annealing prevents internal stress concentration. For fused quartz tubing and components, high-purity feedstocks with trace alkali impurities (Na, K, Li) below 1 ppm are maintained to prevent high-temperature devitrification into cristobalite.
Yes. We support custom color matching, multi-tone calacatta veining, and specialized surface finishes (polished, honed, leathered, brushed). Slabs can be specified up to jumbo sizes of 3250 × 1650 mm. For industrial quartz glass tubes and rings, we produce customized diameters from 3 mm up to 500 mm OD, with client laser-etched batch identifiers and custom packaging.
Every shipment undergo strict multi-stage testing: helium mass-spectrometer leak detection for sealed vacuum apparatus, optical polariscope stress inspection, hydrostatic pressure load testing, ultrasonic dimensional verification, and color-uniformity spectrophotometry against master client-approved swatches.
For custom manufactured artificial quartz slabs and contract architectural runs, standard container-load MOQs apply (typically 1 × 20GP container, approx. 7-8 A-frames), with production lead times of 15-20 days. For custom high-precision quartz furnace tubes and laboratory ware, we accommodate lower MOQ sample prototypes with expedited 7-10 day turnaround.
Explore our comprehensive portfolio of high-temperature quartz components, fused silica plates, and precision rods fabricated for worldwide export.